有限公司控制器英文说明书(英文面板)概要1
CNC-220SUserManual
VER. C-220 0266/0268/0288/0399/ect.
迈维自動化有限公司maiweiAUTOMATION CO.,L TD.
CONTENTS
1. INTRODUCTION. . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .. . . . . . . . . . . . . . .2
2.MAIN FEATURES. . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .. . . . . . . . . . . . . . ..2
3.FRONT PANEL DESCRIPTION. . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .3
4.PROGRAMMINGWINGING PARAMETER. . . . . . . . . . . . . .5
5.WINDING METHOD DESCRIPTION. . . . . . . . . . . . . . . . . . . . . . . .6
6.WINDING EXECUTION. . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .. . . . . . . . .8
7.CONFIGURATION SETTING. . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .9
8. INSTALLATION AND WIRING. . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .11
9.ADJUSTMENT. . . . . . . . . . . . . . . . . . . . . . . . . . . . .. . . . . . . . . . . . . . .. . . . . . . . . . . .14
10.MAINTAINAND TROUBLESHOOTING. . . . . . . . . . . . . . . . .15
迈维自動化有限公司maiweiAUTOMATION CO.,LTD.
CNC-220S isaseriesof COILWINDING MACHINE CONTROLLERdeveloped by MAIWEI AUTOMATION. It notonly retains al l the features ofprevious designs, italso has a low noise level and is less sensitive to externalpower fluctuation.
CNC-220S also features an integrated design:putting stepper motor driver,
DC motorspeed control ler,brake and powersuppl iercontrol circuits into onecontrol box,simultaneously achieving size reduction, high performance andlow cost.
CNC-220S Seriesoffers CNC-220S“Standard Model”and CNC-220S EXD
"External Connection Model”,depending on whethera close-loop driver isprovided for various appl ications.
2.MAIN FEATURES
◆ Single chip DSP Microprocessor design, has further higher performance and higherfunctions; it also has less sensitive to external power fluctuation orto external electromagnetic interference.
◆ Memory capacity capable storing up to 0- 1000 steps winding data,9 winding parameters,and 5 options can be independentlyassigned for each step.Off-power memory retention without battery.
◆ Winding speed can be specified using the front panel keypad, resulting ineasy programming of multi-step,multi-speed settings.
◆ Guiding traverse shaft stepper motor with a constant-current driver offeringfast wire guiding speeds.
◆Power input AC100V~120V、220V~240V 600VA(max).
迈维自動化有限公司maiweiAUTOMATION CO.,LTD.
3.FRONT PANEL DESCRIPTION
3.1.Power switch
Power Powersuppl ier equipped,controls the AC power to the control ler.
3.2.Key pads
0-9 10 key, for entering numerical values.
『QTY SET』 Enter i nto EDIT mode.
『EDIT』 Specifytarget production quantity.
『START STEP』 Specifystarting step in memory.
『END STEP』 Specifyending step in memory.
『DATA SEL』 Select parameter to be programmed,or to switch display mode.『FEED DIR』 Selectguiding direction foreach step.
『WIND DIR』 Selectwinding direction for each step.
『EDGE STOP』 To specifywhether to suspend winding when the guiding traversemoves to the two edges of the width.
『AUTO HOME』 Selectwhether to have auto-positioning function foreach step.『AUTO START』 Selectwhether to have auto-starting function for each step.『-』 Reduce step number byone,or reduce PIECE COUNTER byone.
『CLR』 During programming,clearcurrent data to zero.
『COPY』 Copythe data of previous step i nto current step.
『ENT』 Write data into memory.
『RPM』 Switchdisplayto shows PIECE COUNTor RPM.
『ZERO』 Hold down this keyfor two seconds to reset PIECE COUNTER to zero.『AUTO』 To switch between AUTO and NON-AUTO mode.
『BRAKE』 Switch whether brake wi l l be appl ied to the win spindle during stopping.
迈维自動化有限公司maiweiAUTOMATION CO.,LTD.
『NEXT』 Skip current step and go to the next step.
『PREV IOUS』 Discard currentstep and go to the previous step
『RESET』 At any time,discontinues current operation and return to ready mode.
『STOP』 Pause during winding.
『START』 Restart during pause,or pause during wi nding.
.
.
3.3.Digital display
Procedures displayer Show the currentstep number being wound or being
Documents displayer During programming, in combination with LED,shows theparameter being programmed.During winding or ready mode,show thecurrent numberof turns or show the guiding traverse shafts position.
Qtydisplayer Shows PIECE COUNTor RPM.
3.4.Status indicators
□ READY: l it means in READY mode, flash means PAUSE mode,not l itmeans winding or programming in progress.
□ RUN: l it means winding in progress; not l it means not in progress.
□SLOW:during winding, l it means low speed winding; not l it means highspeed winding.
□ MOVE: l it means guiding traverse is fixing the starting position forwinding or is returning to the home position.
□ O.S: l it means winding operation is overspeeding,guiding traverseand winding spindle shaft are out of synchronization.
□ LAN: l it means currently communicati ng with network.
□ FINISH:wi l l l itwhen reaching the preset piece count.
□RPM: l itmeans the PIECE COUNTDISPLAYshows RPM.
□QTY: l itmeans the PIECE COUNTDISPLAYshowsthe piece count.
迈维自動化有限公司maiweiAUTOMATION CO.,LTD.
3.5.Winding parameters definitions
□SHIFT:Starting position of the guiding traverse.
[Setting range 0.00~999.99 mm].
□WIDTH :The traverse of the copper wire led by the traverse duringwinding. [Setti ng range 0~999.99 mm].
□PITCH:Diameterof the copper wire. [Setting range 0~9.999mm].
□TURNS:Total number of turns to be wound.
[Setting range 0.0~9999.9 or 0~99999 turns] .
□S.SLOW:Number of turns to be wound at low speed,when start winding.
[Setting range 0~999.9 turns].
□E.SLOW:Number of turns to be done at lowspeed prior to stopping.
[Setting range 0~999.9 turns].
□H.S. :High winding speed. [Setting range from 0~99%].
□L.S. : Low winding speed. [Setti ng range from 0~25%].
□FUN :Winding complete output signal setting.
4.PROGRAMMINGWINGING PARAMETER
4.1.MEMORY RANGE SELECTION
CNC-220S contains 1000 memorystep,By defining the region, users caneffectively manage the memory.Various winding parametercan be stored indifferent regions and can be retrieved instantaneously.After specifying theregions,programming and winding can be done in those regions;al lun-selected regions wi l l retain their original contents and unmodified.Whensetting the STEP number, the Ending step numbermustbe larger than the
Starting step number,or the winding operation wi l l notstart
Specifying starting step
In ready mode,press to select. [Setting range 0~999].
Specifying ending step
In ready mode,press to select. [Setting range 0~999].
4.2.Programming winding parameter
In“READY”mode,press invokes the programming mode.First the
“START STEP”number wi l l shows at “Procedures displayer” , the parameter indicator『SHIFT』wi l l l it, the starting position wi l l shows at “Documents dispayer” .Thestarting position can be changed to the new position bypressing thenumerical keys fol lowed bythe key.
After that the STEP number wi l l automatical ly increase by one, to continue setthe starting position for nextstep.When the STEP number larger then the
“END STEP” number, the STEP number wi l l restore to the “START STEP”number and the indicator l ight wi l l change from『SHIFT』 to 『WIDTH』 foruser to specifying the width for each STEP.Repeat the same procedure usingnumerical keys and the key,al l winding parameters for each STEP canthus programmed,after that press key again to go back to readymode.
迈维自動化有限公司maiweiAUTOMATION CO.,LTD.
.
.
.
.
Eachtime whenchange the PARAMETERor OPTIONS, keymustpressed to effect the change.
4.3.Guiding traverse shaft introduce setting
During set the 『SHIFT』 , 『WIDTH』 and 『guiding traverse travel l imit』 ,can use numeric keypad to set location data or can also useTo leading the guiding traverse shaft location.
4.4.Clear all winding parameter
In the”READY”mode,press wi l l clear al l the winding parameter inthe memory.Be cautious in using this function or al l the data wi l l be lost.
5.WINDING METHOD DESCRIPTION
Priorto winding, the general winding principles are explained belowso theoperators can have a better understanding of the performance of thecontrol lerand make better use of it.
5.1.Counting mode
(Refer to the section 7.1 .Counting mode).
◆Absolute counting mode
Winding spindle shaft is capable of fixed-pointstopping.Upon each restart,
迈维自動化有限公司maiweiAUTOMATION CO.,LTD.
the turn count wi l l resetonly the integer portion of the turn’s to zero,with thedecimal unchanged.Forexample, for a previous number of 100.3 turns,whenrestarting the next step winding, the counting wi l l start with 0.3 turn to avoidaccumulation of spindle shaft free play errorfrom consecutive windings.Thiscounting method may cause insufficient winding by one turn.Therefore,whenstarting from 0.5~0.9, the spindle wi l l turn to the 0.0 before it starts counting.
◆Relative counting mode
This counting method zeros the counter upon each restart, therefore it is easyto understand and wi l l not cause i nsufficient winding.
5.2.Wire-guiding mode
◆Interlace wire-guiding
If the 『幅宽』 of the step is zero, the wire-guiding becomes interlace mode.When it begins winding, the wire-guiding wi l l fol low the wire direction toproceed two wire diameters and regress one wire diameters cycl ical ly unti l thestep of winding ends.This mode especial ly suits the inductor winding.
◆Non wire-guiding
Sometimes, the winding device may be used to winding adhesive tapes orcopperfoi l .Whenthe wire-guiding is not needed, 『PITCH』may be adjustedto zero and the wire-guiding won'tbe move.
5.3.Operation mode
(Refer to the section 7.1 .Operation mode).
◆Singleclick mode
When press the start switch, the motor start winding,and when you releasethe start switch, the motor stop windi ng immediately.
◆Doubleclickmode
When press the start switch, the motor start windi ng,and if you want to pausethe motor,you have to release the start switch then press it again.
5.4.Running mode
◆Continualmode
Before it begins winding, if 『SHIFT』 of the step set as 999.99, then the startingposition, the width, the wire-guiding direction and the winding direction won'tbe re-read.The values are not changed, that is the wire guiding wi l l continueguiding wires on the same position.The width and left-right margins are thesame as the ones of the previous section.Both the wire-guiding and windingdirections are notchanged either.This mode especial lysuits to winding whichhave the multiple drawing tops in the same sets of coi ls.
◆Edgesslow mode
The winding speed wi l l slow down before the guiding traverse reach to the twoedges of the width(work with 『E.SLOW』 turns).After the guiding traverse
迈维自動化有限公司maiweiAUTOMATION CO.,LTD.
veered, then restore to hi-speed winding. (Refer to the section 7.1 .edge slowmode).
◆Automatically circularly mode
If keyset to on, it means Automatical ly circularly mode, inthis modewhen finish a step of winding it wi l l automatical ly get into next step and startwinding without press key(work with and keys).
5.5.How to Correct setting turns
◆Preset method
Setthe 『E.SLOW』 to zero first and then set the 『TURNS』 to the desirednumber.Set proper parameters according to copper wire,bobbin, tension,etc,then press to start winding.When finished,obtain the actual number ofturns and calculate the numberof overshot turns.Go into programming modeand subtract the numberof the overshot turns from the 『TURNS』 to obtainthe req uired setting.
This method has a higher throughput, however, the resulting stopping locationmay not be precise.
◆High-Low speed method
This method uses a combination of 『H.S.』 / 『L.S』 and 『E.SLOW』 to achievethe desired numberof turns.
The 『L.S.』 should not be too high.The numberof 『E.SLOW』 turns must beadequate to al low the spindle shaftto slowdown to lowspeed before reachingthe total numberof turns.This can result in precise stopping location.
◆Double-brake method
As the winding turns of the winding shaft reach the numbers of the 『E.SLOW』 ,brake for a short period first.After the winding shaft stops,continue winding atlowspeed.Therefore the numbers of the slowspeed maybe reduced and theefficiencyof winding may be increased, (Refer to the section 7.1 .brakingmode).
6.WINDING EXECUTION
6.1.To startwinding
Afterset up al l data items,press key the winding process begins inaccordance with the set-up content.Press key to pause wi nding.Duringwinding,press the key, the winding speed can be switch between highspeed and low speed.
迈维自動化有限公司maiweiAUTOMATION CO.,LTD.
6.2.Change the display mode
During winding orduring PAUSE mode,press key, the“Documents displayer”canbe change the display mode between turns orguiding traverse position.
6.3.Winding speed(RPM)display
Pressing keywi l l cause the”QTYdisplayer” to displaythe spindleshaft “RPM”without interrupting the counting.Pressing again wi l l change the“QTYdisplayer”backto displaying the piece count.
6.4.Piece counter management
Upon turning on the“POWER”, “QTYdisplayer” wi l l showsthe numberof piece produced.During wining,each time the CONTROLLERgoes from the“Stert step” to the“End step”, the piece counter wi l lautomatical ly increase byone.
◆Preset piece counter
In“ready”mode,press key once and key in desired values fol lowedby the key.When the“QTY displayer”reaches the preset value, the
FINISH led wi l l l it. [Setting range 0~99999] .
◆Decrease piece counter
During“READY”or PAUSE mode,press the keyand hold down for twoseconds the piece counter wi l l decrease by one.
◆Reset piece counter
In any time holding down key fortwo seconds, it wi l l set the piececounter to zero.
7.CONFIGURATION SETTING
CNC-220s is a multi-purpose design, to meet various requirements;additional settings are configured to provide flexibi l ity foradditionalappl ications.
In the “READY“”mode,press the fol low”ing keys combination as section
[7.1.~7.8], the Documents displayer wi l l showcorresponding setting value. If nochange is necessary,press the keyget back to“READY”mode.Orpress keyto get into change mode, then the parametercan be changed by
In this function the STEP displayand the DATAdisplaywi l l shows eight digits,representing eight winding mode selections respectively.
Press numerical keys as below to set each digit.
- 有限公司控制器英文说明书(英文面板)概要1相关文档
- 有限公司控制器英文说明书(英文面板)
- 如图面板灯安装说明书英文 面板灯安装说明书
- 打印爱普生4000面板英文翻译
- 主菜开利30RB涡旋式风冷冷水机组英文面板简单操作
- 面板hypermesh主要面板英文翻译
- 面板hypermesh主要面板英文翻译
易探云服务器怎么过户/转让?云服务器PUSH实操步骤
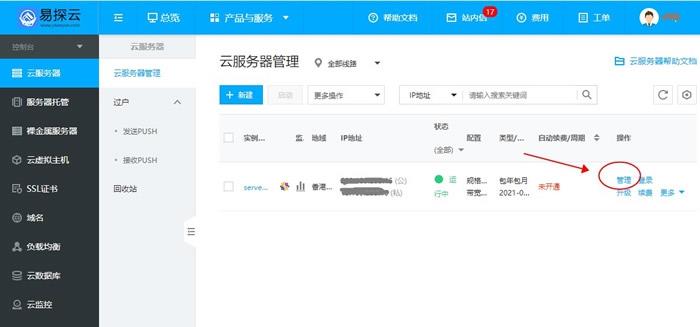
易探云服务器怎么过户/转让?易探云支持云服务器PUSH功能,该功能可将云服务器过户给指定用户。可带价PUSH,收到PUSH请求的用户在接收云服务器的同时,系统会扣除接收方的款项,同时扣除相关手续费,然后将款项打到发送方的账户下。易探云“PUSH服务器”的这一功能,可以让用户将闲置云服务器转让给更多需要购买的用户!易探云服务器怎么过户/PUSH?1.PUSH双方必须为认证用户:2.买家未接收前,卖家...
创梦网络-四川一手资源高防大带宽云服务器,物理机租用,机柜资源,自建防火墙,雅安最高单机700G防护,四川联通1G大带宽8.3W/年,无视UDP攻击,免费防CC
? ? ? ?创梦网络怎么样,创梦网络公司位于四川省达州市,属于四川本地企业,资质齐全,IDC/ISP均有,从创梦网络这边租的服务器均可以****,属于一手资源,高防机柜、大带宽、高防IP业务,另外创梦网络近期还会上线四川联通大带宽,四川联通高防IP,一手整CIP段,四川电信,联通高防机柜,CN2专线相关业务。成都优化线路,机柜租用、服务器云服务器租用,适合建站做游戏,不须要在套CDN,全国访问快...

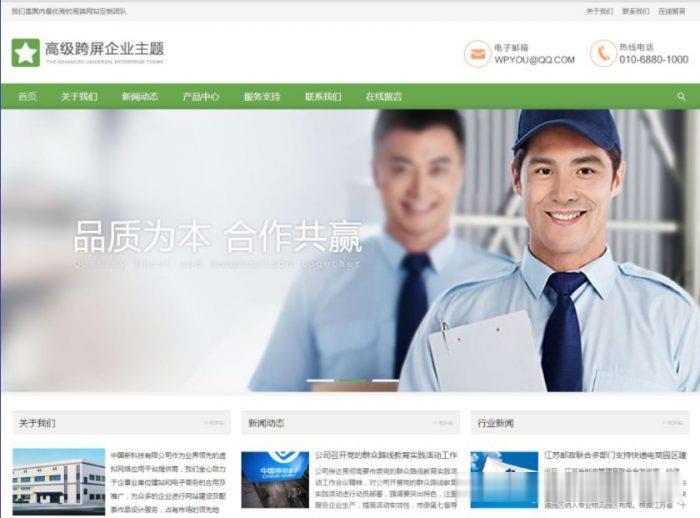
wordpress高级跨屏企业主题 wordpress绿色企业自适应主题
wordpress高级跨屏企业主题,通用响应式跨平台站点开发,自适应PC端+各移动端屏幕设备,高级可视化自定义设置模块+高效的企业站搜索优化。wordpress绿色企业自适应主题采用标准的HTML5+CSS3语言开发,兼容当下的各种主流浏览器: IE 6+(以及类似360、遨游等基于IE内核的)、Firefox、Google Chrome、Safari、Opera等;同时支持移动终端的常用浏览器应...
-
苏州商标注册苏州如何申请商标注册?推广方法最有效的推广方法是什么?arm开发板ARM开发板和树莓派有什么区别今日热点怎么删除怎样删除实时热点网易公开课怎么下载手机上的网易公开课的付费课程怎么下载??????神雕侠侣礼包大全神雕侠侣手游华山论剑礼包有什么 怎么领取数据库损坏数据库坏了,怎么修复?xp系统停止服务Windowsxp系统为什么停止服务二层交换机集线器和二层交换机,三层交换机的区别网络广告投放网络广告的投放目的是什么?